Wyman-Gordon Lincoln
Wyman-Gordon’s Lincoln has Europe’s largest counterblow hammer (900KJ) at the heart of the operation.
About
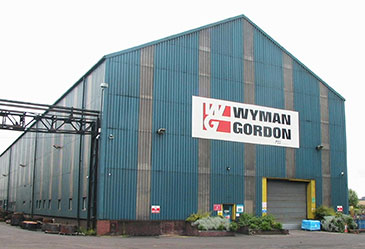
Wyman-Gordon’s Lincoln facility, located in England, UK, supplies forged products globally to the aerospace and energy markets.
The DG90 hammer is capable of manufacturing hot die forging of Aerospace, Powergen, Oil & Gas and Nuclear components (asymmetric forgings, discs, shafts and valve bodies). It is the largest of its type in Europe, forging at temperatures of up to 1340°C.
Smaller components are manufactured on the 400KJ DG40 counterblow hammer. Both counterblow hammers are fully computer controlled to ensure repeatability of the process. The 2 counterblow hammers are supported by a Zdas 630T CNC controlled pull down press which is utilized in the manufacture of pre-forms for asymmetric structural parts and long aero engine shafts.
From Smith-Clayton Forge to Wyman-Gordon
Smith-Clayton Forge was established in 1929 in Lincoln for the manufacture of aerospace and automotive forged products for a cost of £50,000. In 1956 the DG40, the first of the 2 counterblow hammers, was installed, followed by the DG80 in 1970. The DG80 was uprated to DG90 in 2008.
In May 2000 the Aerospace Division of what was then known as UEF was acquired by Precision Castparts Corp. and incorporated into the Wyman-Gordon Forging Division.
Today, the Lincoln facility works in unison with sister plants in Livingston, UK, and Plzen, Czech Republic, to provide a diverse range of machined forgings serving customers globally.
Products
Manufacture of Compressor, Turbine & Fan Disks, valve bodies, and shafts.
| Product | Weight | Material |
|---|---|---|
| Engine Fan Disk | 1,300 lbs | Ti-17 |
| LPT Disk | 1,200 lbs | Inco-718 |
| LPT Disk | 1,500 lbs | Inco-718 |
| Product | Weight | Material |
|---|---|---|
| IGT Turbine Disk | 10,000 lbs | — |
| IGT Turbine Disk | 12,000 lbs | Inco-706 |
| IGT Spacer | 20,000 lbs | Inco-706 |
Equipment & Capabilities
Equipment
Forgings
Materials
From Forging to Final Inspection
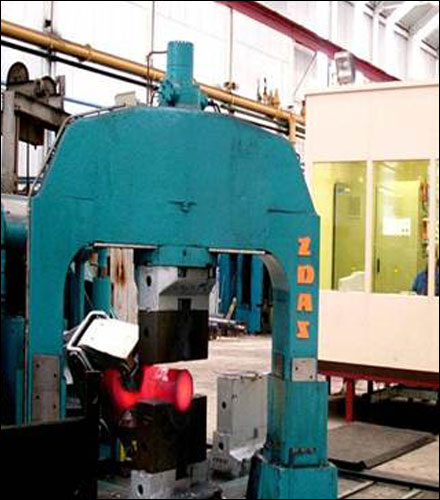
Shafts are forged on the ZDAS 630T Pull-Down Press with a 3T computer controlled manipulator. This is supported by an upsetting press for flanged shafts.
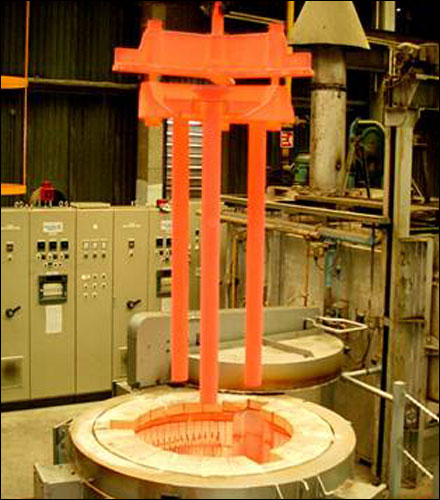
Shafts are heat treated in our specialized vertical heat treatment furnaces with vertical flood quenching capability. This ensures minimal distortion from the heat treatment process. The heat treatment process is capable of heat treating shafts up to 9′ long and 20″ in diameter.
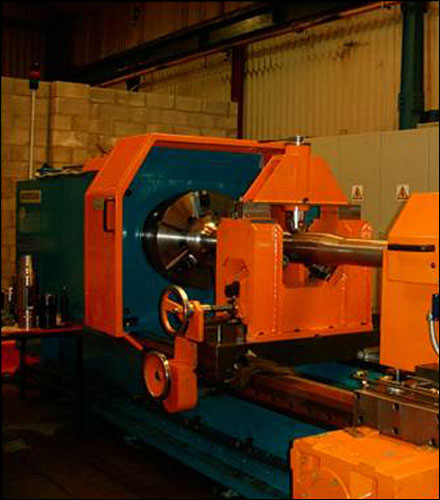
The deep hole boring process is specifically designed to machine bores through shafts at maximum metal removal rates. This process is used for both pre and post heat treat operations.
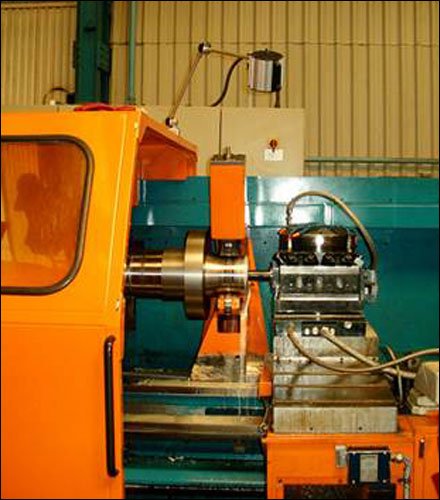
Working in conjunction with the deep hole borer, these machines are used to pre and post heat treat machine shafts up to 9′ long and 20″ in diameter.
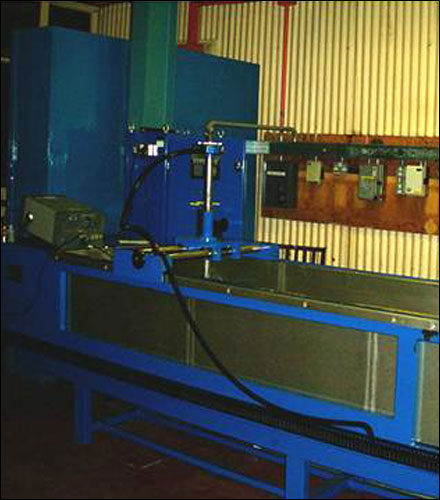
Shafts are ultrasonically tested using immersion ultrasonic techniques.
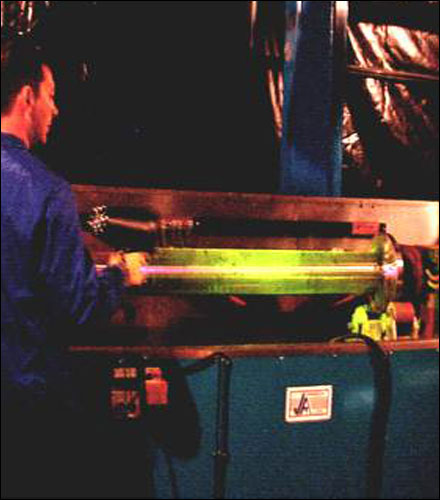
Magnetic particle inspection technique is used to check for surface imperfections.
Plant & Engineering
PRI-NADCAP special process approvals for heat treat, penetrant & chemical processing, and mag particle inspection.
The 900KJ and 400KJ hammers are both utilized to manufacture closed-die forgings for aero engine, IGT and airframe markets worldwide. In addition, specialist industrial, nuclear, and automotive products such as large connecting rods and valve bodies are also forged. The Zdas 630T pull down press is utilized to forge long aero engine shafts and asymmetric preforms for subsequent closed-die forging on the counterblow hammers.
Ready to Start Your Project?
Contact our team to discuss your requirements, or request a quote to get started.